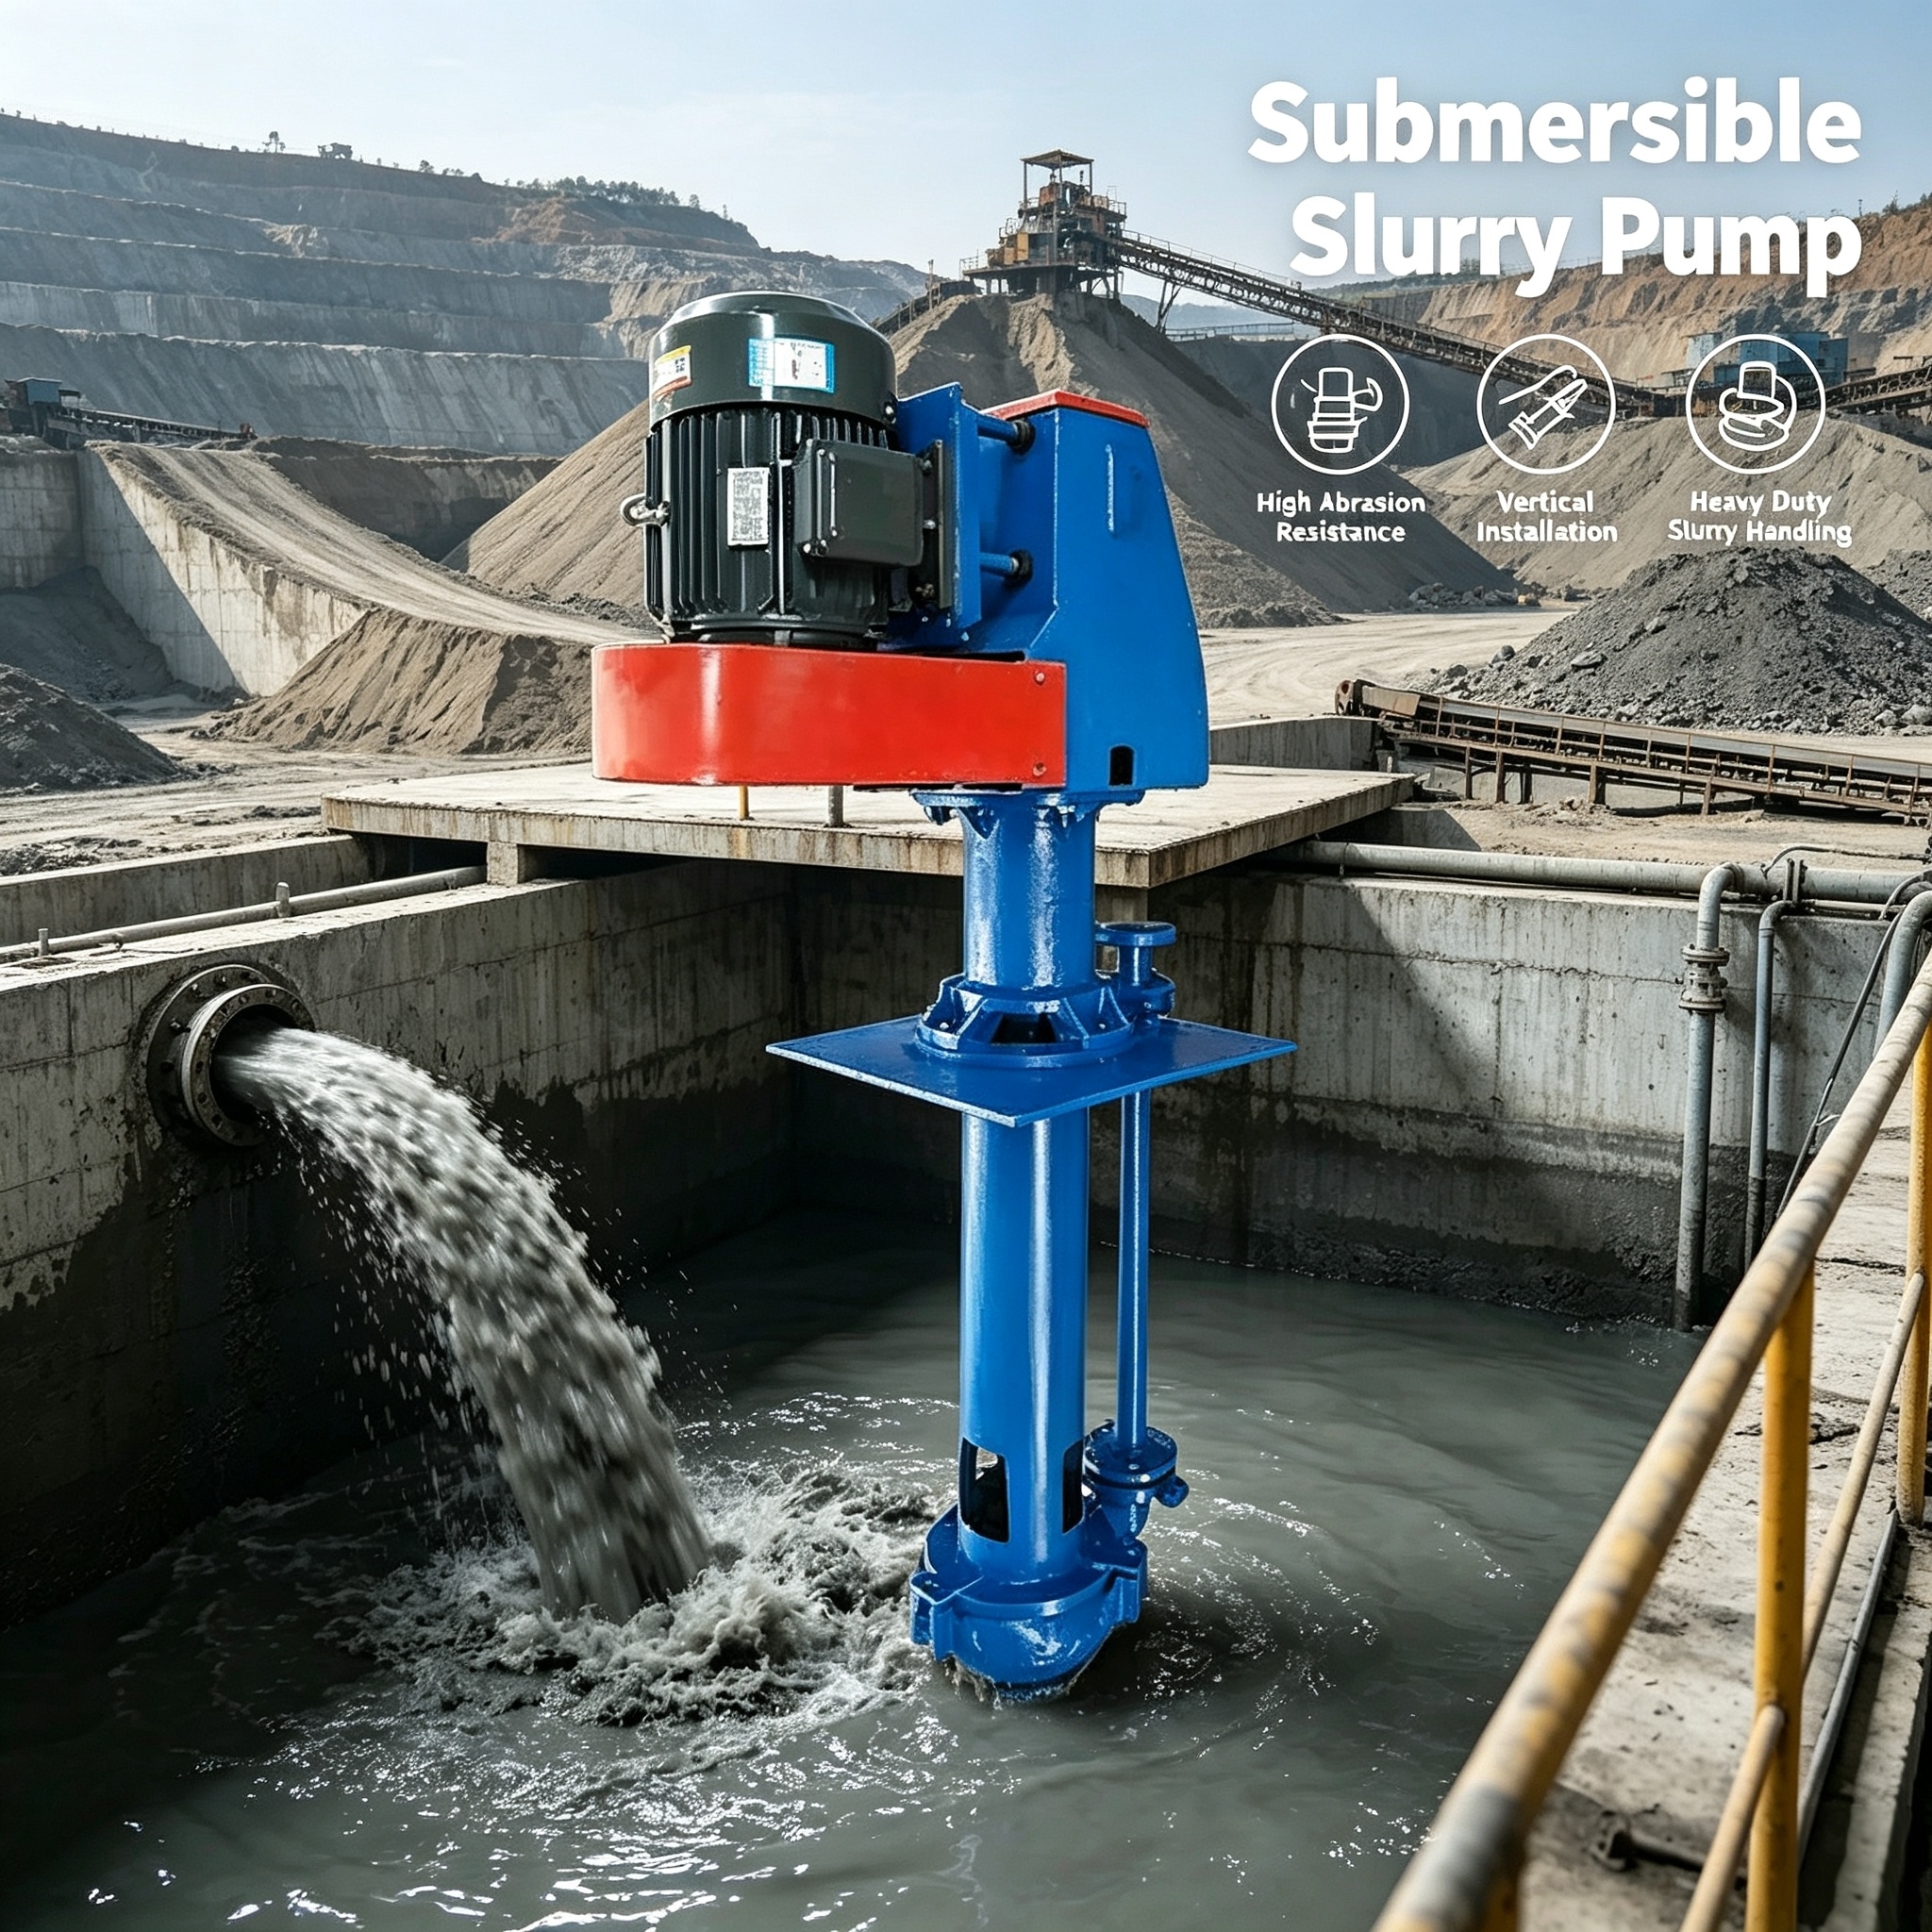
ZJQ Submersible Slurry Pump | Zero Auxil...
Oct 06, 2026
Core Technical Advantages
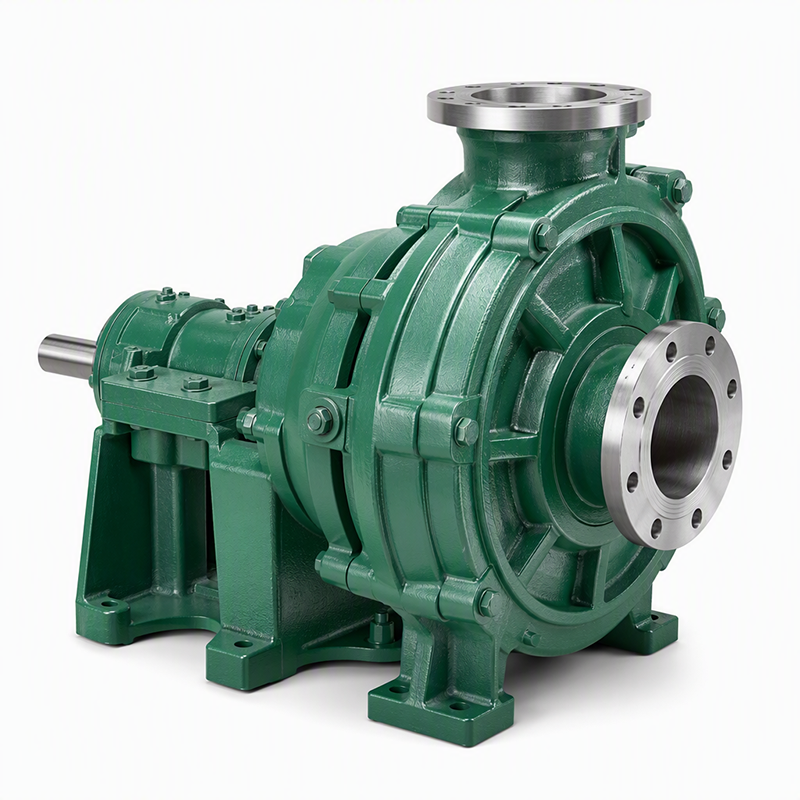
Dual Liner Solutions for Full-Condition Adaptability The AH slurry pump supports high-chrome metal lining and natural rubber lining interchangeably. Metal lined models excel in coarse particle, high-impact and ultra-abrasive ore slurry scenarios. Rubber lined versions provide excellent corrosion resistance and fine-particle anti-erosion performance for chemical and medium-abrasion slurry. This dual-structure design enables precise matching for different media, greatly extending service life in complex working environments.
Heavy-Duty Split Casing & Reinforced Bearing System Adopting axial split casing structure, the upper cover can be opened directly for quick replacement of liners, impellers and seals without dismantling pipelines. Equipped with oversized heavy-duty bearing assembly and rigid bracket, the pump maintains low vibration and stable operation under maximum load and high thrust conditions, avoiding shaft swing and component damage during long-cycle operation.
Optimized Wide Flow Channel Anti-Clog Hydraulics The AH series features a large unobstructed flow passage and wide-blade impeller design. It effectively reduces particle blocking and flow turbulence, allowing smooth passage of gravel, ore chunks and high-density slurry mixtures. Even under unstable particle size and fluctuating concentration, the pump maintains continuous and uniform conveying capacity.
Excellent Continuous Load Capacity for Industrial Process Engineered for true 247 heavy-duty operation, the AH pump features strong overload resistance and stable hydraulic curve. It adapts to frequent flow and pressure changes in mineral processing circuits, tailings pipeline transportation and coal washing circulation systems, ensuring zero production interruption caused by pump failure.
High Compatibility & Easy Maintenance Standardized modular structure ensures high interchangeability of spare parts. Multiple transmission methods including belt drive, direct coupling and reducer drive are available to match different power and speed requirements. Simple disassembly and universal accessory standards greatly reduce on-site maintenance difficulty and inventory costs.
Main Application Fields
Mineral processing plant grading and circulation, coal washing heavy-medium separation, mine tailings long-distance pipeline transportation, thermal power plant ash and slag removal, metallurgical residue processing, quarry sand and gravel pumping, chemical abrasive sludge treatment and large-scale industrial continuous slurry conveying systems.
Manufacturer Strength & Global Service
All AH heavy-duty slurry pumps undergo strict hydraulic performance testing, wear resistance inspection and continuous load aging tests before delivery. We provide professional model selection, material customization, transmission scheme optimization and complete spare parts supply. Full lifecycle after-sales technical support is available for global mining enterprises, engineering contractors and industrial pump distributors.